Enstark Logo
CNC Punching Services

CNC Punching Services

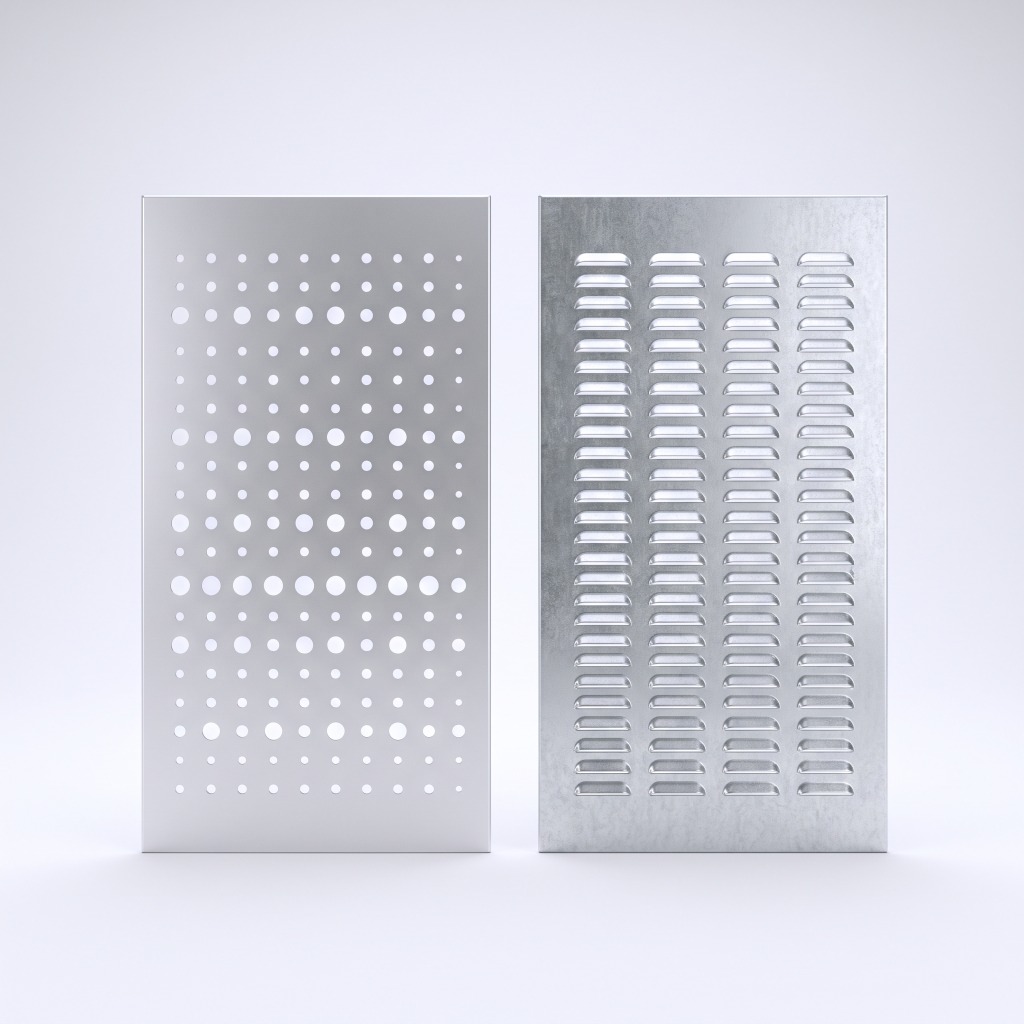
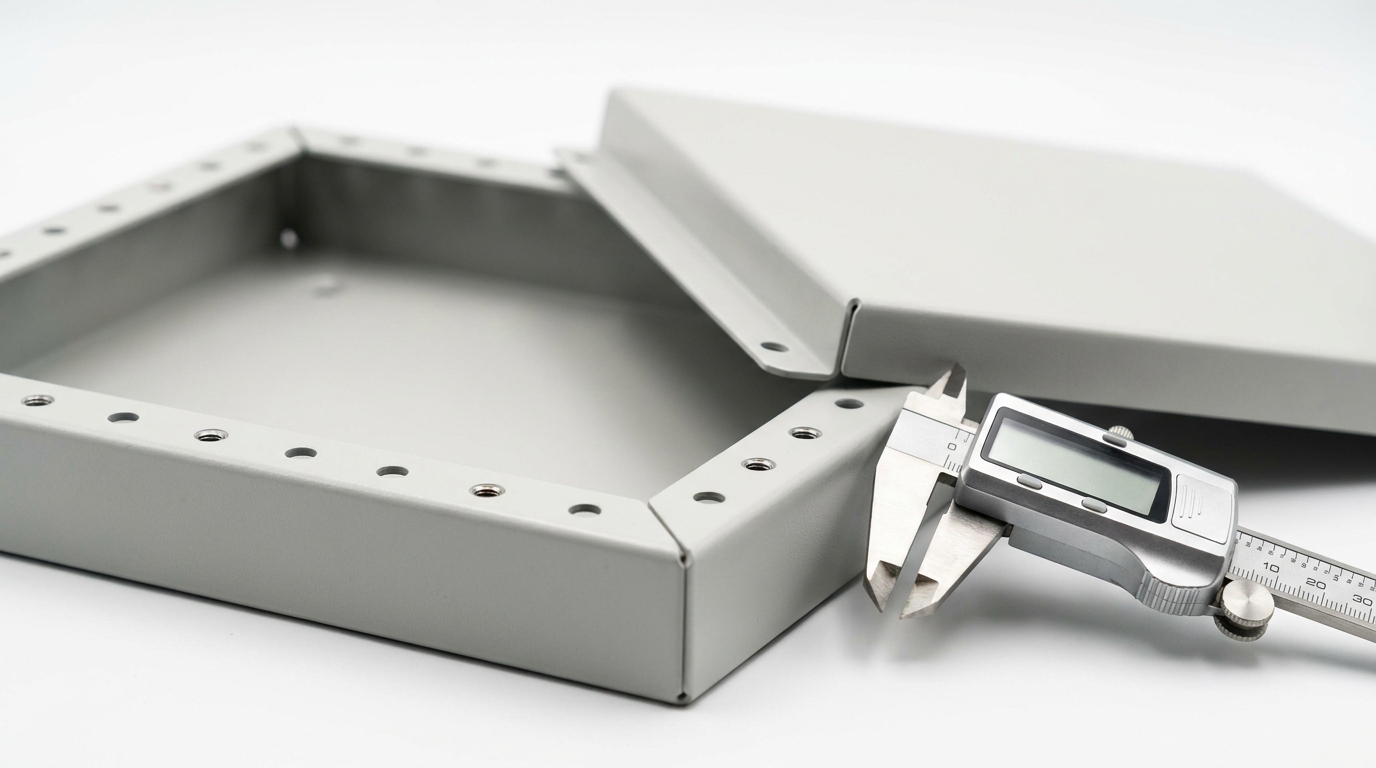
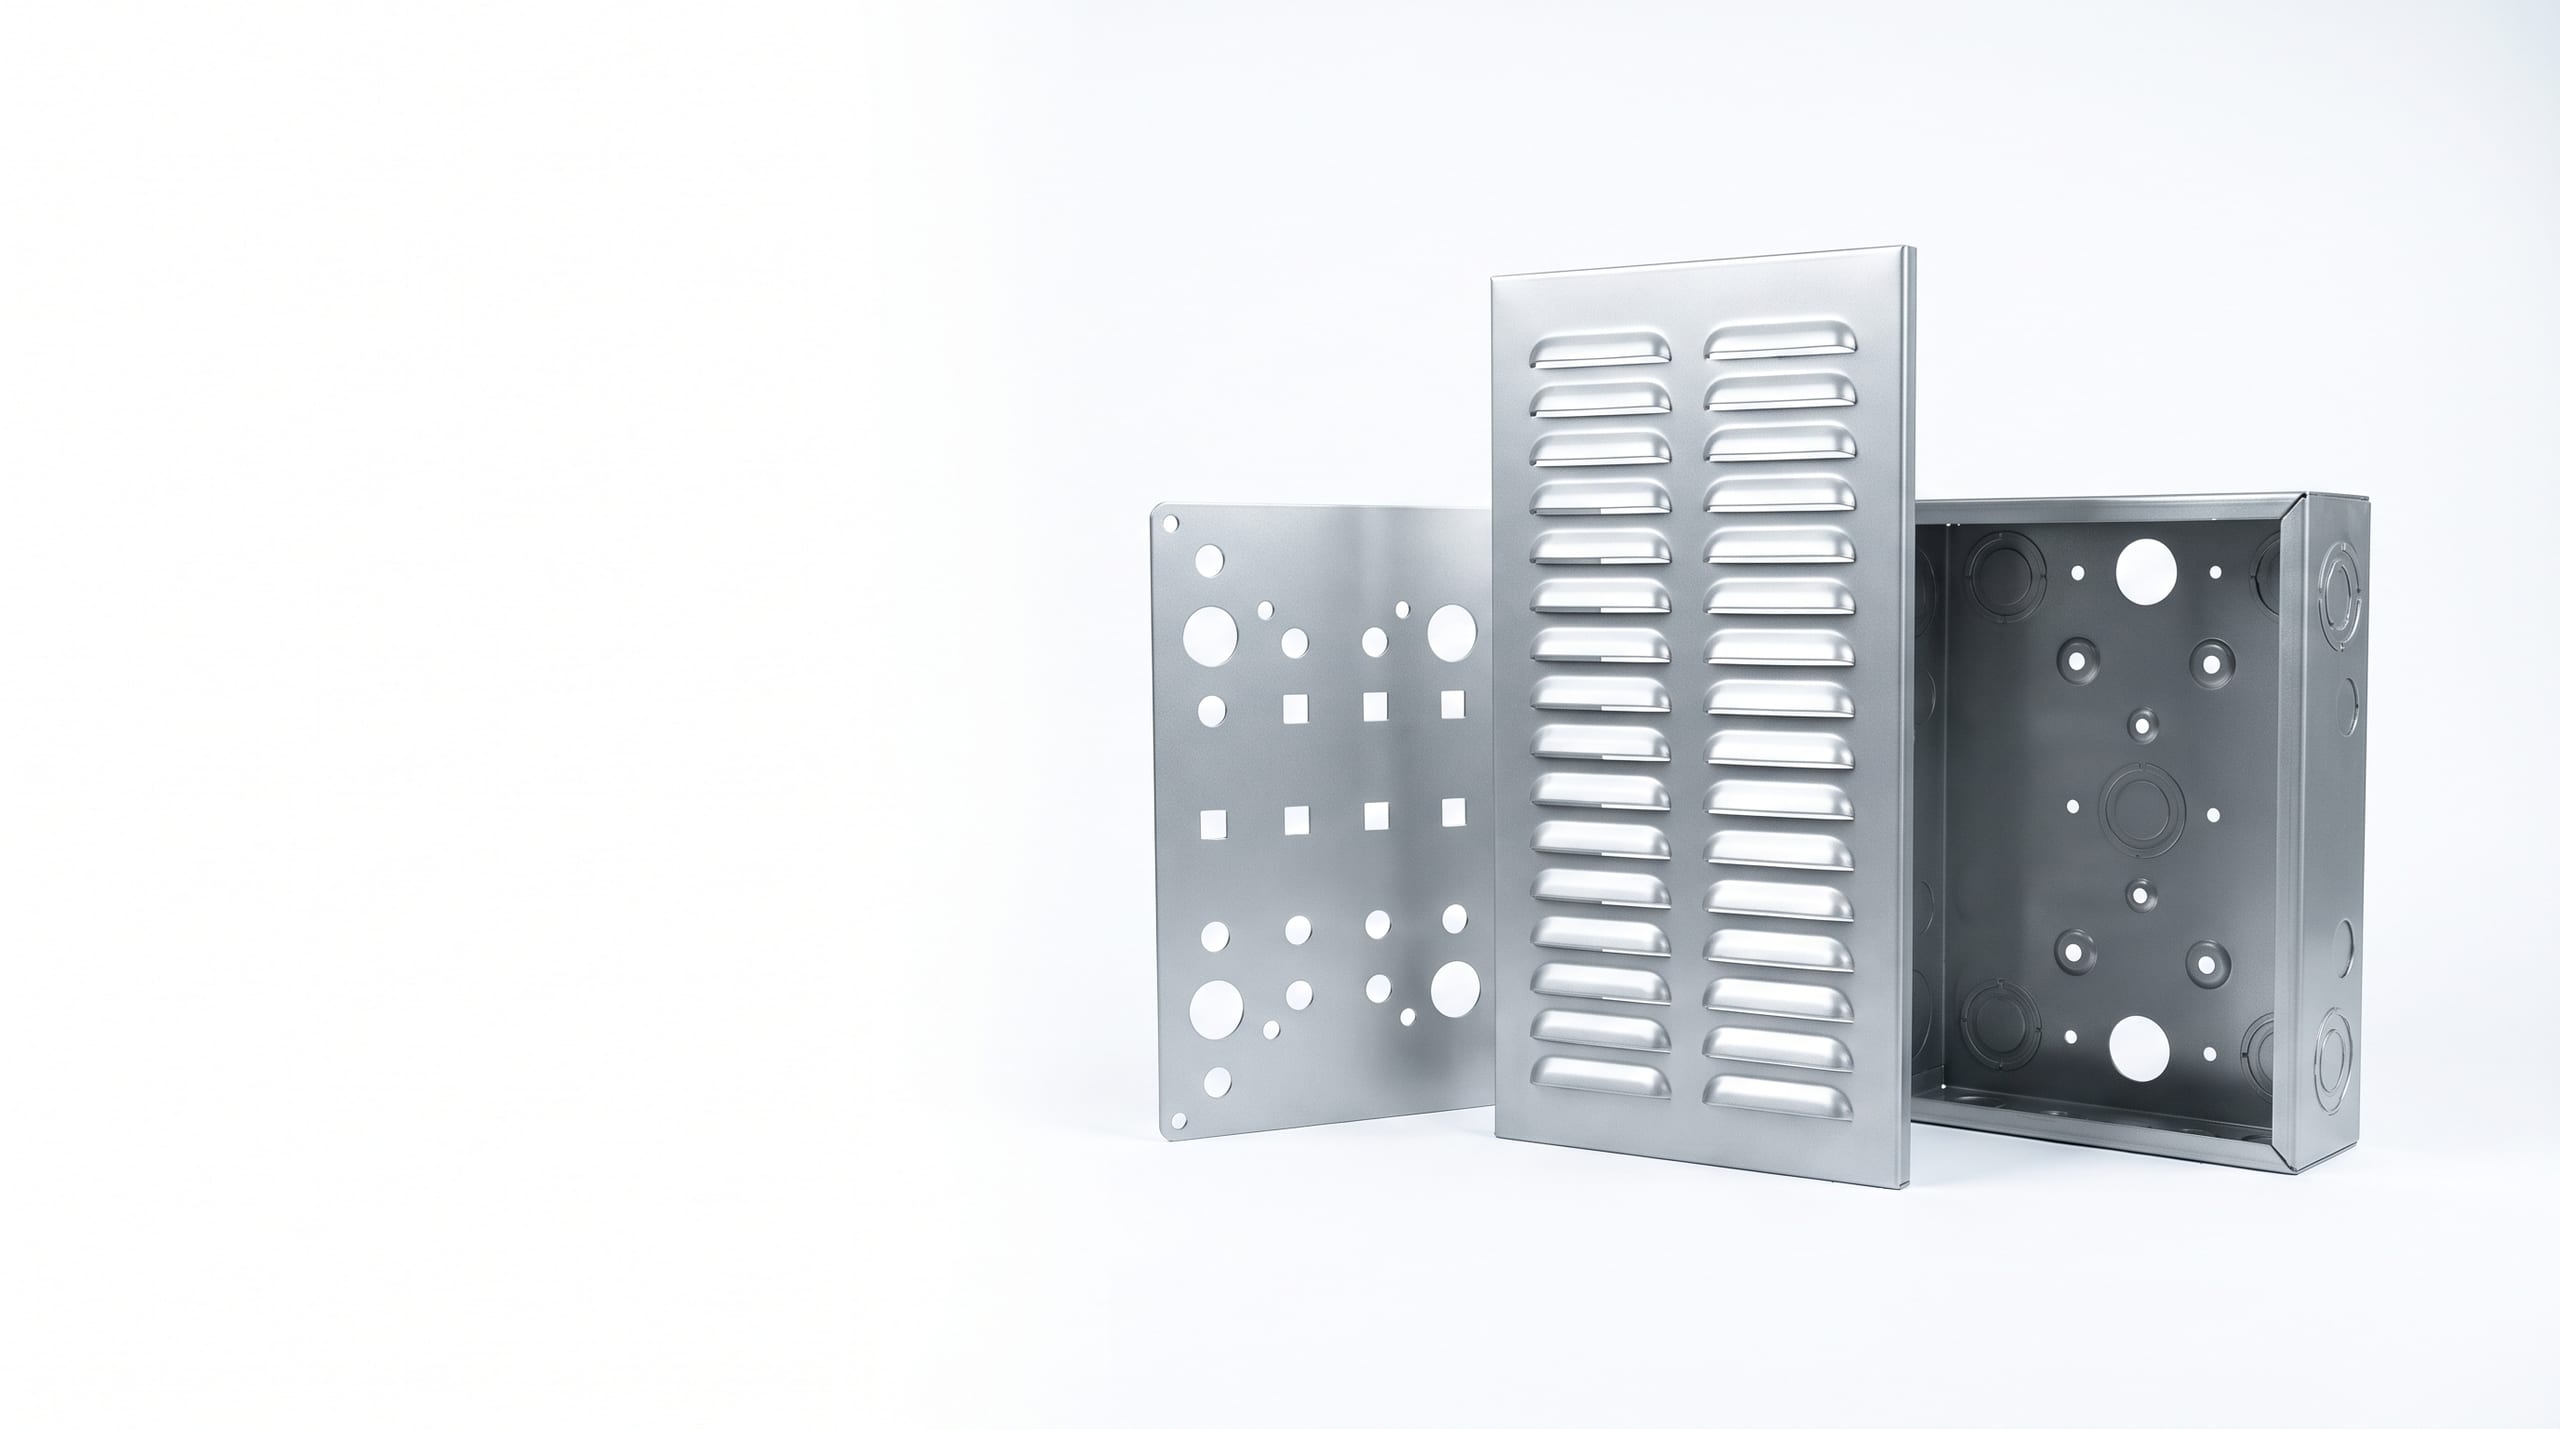
Enstark punches holes, slots, louvers, knockouts and embossed features into sheet metal on CNC turret presses. It is the fastest, lowest-cost way to produce hole-heavy panels, from prototypes to large production runs.

✓
100,000+ Parts Made
✓
ISO 9001:2015 Certified
✓
Parts in 3–5 Days

Get an Instant CNC Punching Quote

Upload your CAD file for instant pricing and DFM feedback.
Drag & drop CAD files hereSTEP, STP, STL, IGS, IGES, PDF, ZIP — up to 15MB
No commitment required · DFM feedback included
Huawei Technologies
Samsung Electronics
Tata Motors
Delta Electronics
Lens Technology
Eveready Industries
Beijing Institute of Technology
Ansell LTD
NRTC
Chantelle
PT Wings Surya
PT Sun Paper Source
PT Supreme Paper Solution
Huawei Technologies
Samsung Electronics
Tata Motors
Delta Electronics
Lens Technology
Eveready Industries
Beijing Institute of Technology
Ansell LTD
NRTC
Chantelle
PT Wings Surya
PT Sun Paper Source
PT Supreme Paper Solution
Design Guide
Max dimension2500 × 1250 mm sheet
Material Thickness0.5–3 mm
Tolerances±0.1 mm or ±0.004"
Wall Thickness / Radius
1× material thickness min hole diameter (1.2× for stainless)
Min Feature Size
1.5× thickness between holes; 2× thickness to edge
Surface Finish Options
As-punched, deburred, tumbled, tapped, powder coated, plated, anodized
Design advice
1/ Standardize hole diametersConsolidating hole sizes reduces the number of turret tool stations needed, minimizing setup time and lowering unit costs.
2/ Orient formed features in one directionKeep louvers, knockouts, and embosses facing the same side of the sheet to avoid collisions with press clamps and dies.
3/ Space formed features adequatelyMaintain clearance of at least half the tool station diameter between formed features to avoid sheet warping.

Punching Materials

Turret punching performs exceptionally on thin-to-medium sheet metals with high punch cycle rates.
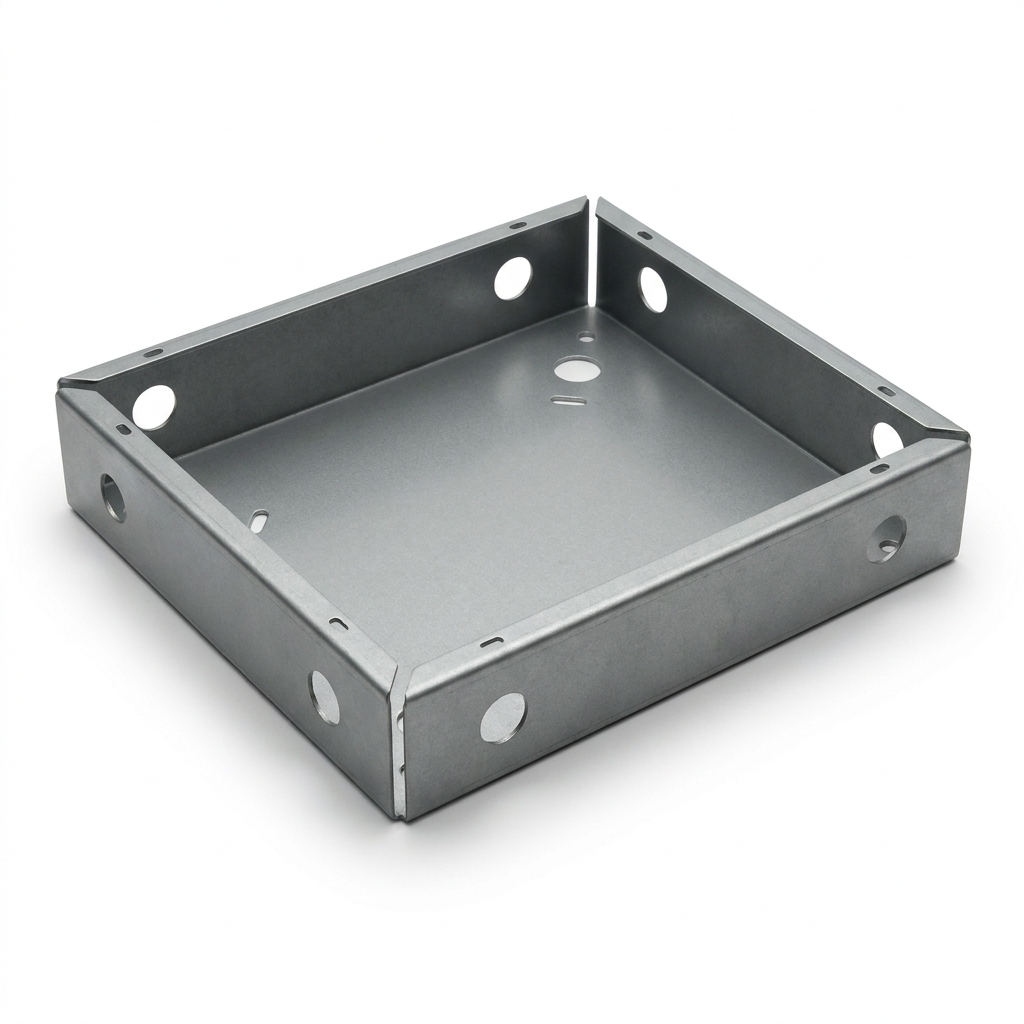
Cold-Rolled Steel (SPCC / 1008)
The most economical punching material. Shears cleanly with minimal burrs and accepts powder coating readily. Used for equipment chassis and panels.
Dark Gray
Appearance
$
Price Rating
From 3 business days
Lead Time
Cold-Rolled Steel (SPCC / 1008)
Enstark operates fiber lasers, multi-axis CNC press brakes, turret punches, and robotic welding cells under one unified ISO 9001 quality system.Why Enstark for CNC PunchingEvery file undergoes upfront DFM review to verify hole-to-edge spacing, bend allowances, and tooling clearances before production starts.
300+Sets of Machine
120+Countries Shipped
20k+Customers Served
Global Shipping World Map
Enstark Online Custom Sheet Metal Service SolutionsGet Quote
Laser Cutting/01
For freeform outer profiles or non-standard contours beyond turret tooling, fiber lasers cut to ±0.1 mm with zero tooling investment.
Laser Cutting Solution
CNC Bending/02
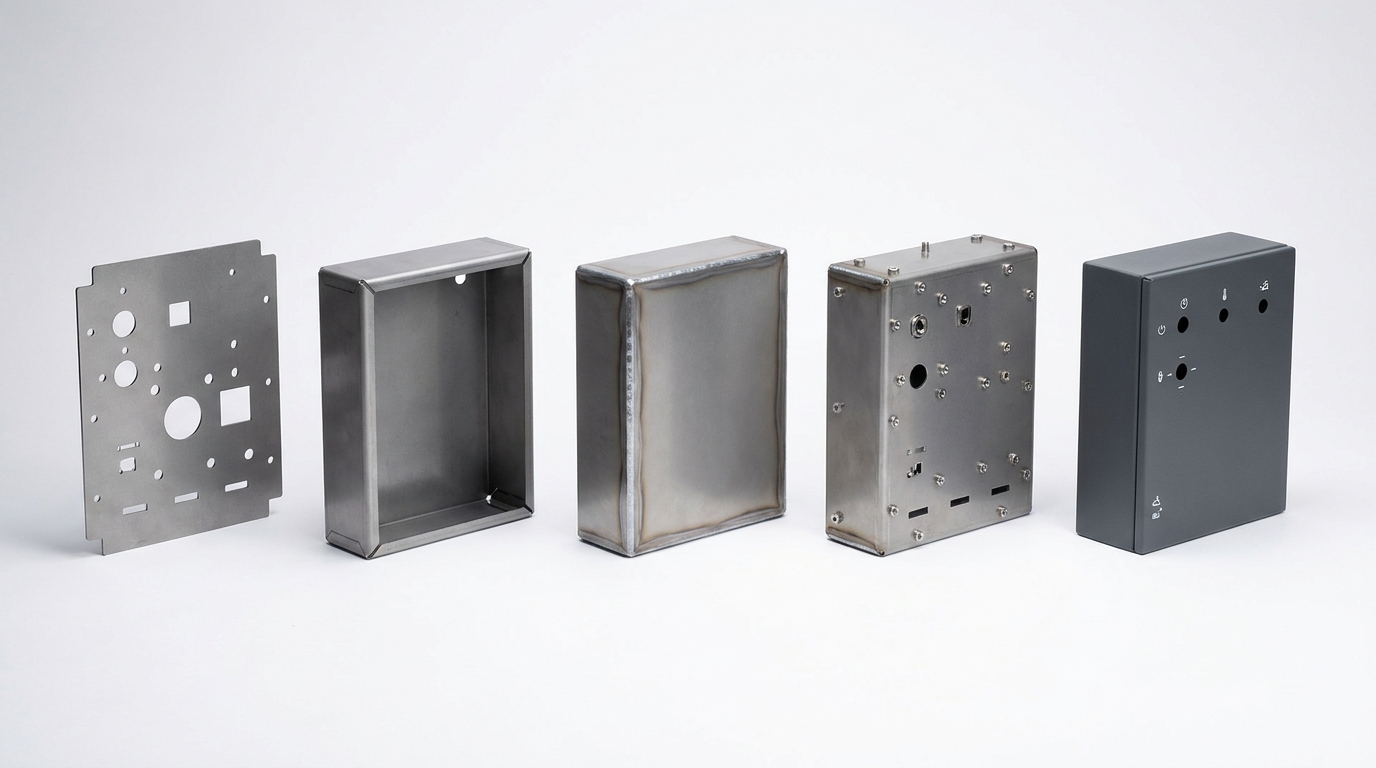
Fold punched blanks into vented chassis, U-channels, and bracket enclosures on CNC press brakes with ±1° angle control.
CNC Bending
Sheet Metal Enclosures/03
Turnkey punched and bent electronic cabinets outfitted with louvers, knockouts, PEM hardware, and powder-coated finishes.
Sheet Metal Enclosures

Punched Part Post-Processing Capabilities

Post-punching deburring, threading, and protective finishing capabilities.

Scroll horizontally to view finishes →
Finishing Process
Surface Roughness
Dimensional Change
Primary Application / Benefit
As-Punched (no finishing)
Burr height up to 10% thickness
None
Internal enclosed brackets and non-handled parts
Vibratory Deburring
Ra 1.6–3.2 µm on edges
−0.05 to −0.1 mm on edges
Removes sheared burrs for safe handling and clean gasket fits
Rotary Tumbling
Ra 0.8–1.6 µm
−0.02 to −0.05 mm
Smooth radius on small punched components in batch volumes
Tapping & Countersinking
ISO metric standard
Adds threads or 90° chamfers
Direct screw fastening without loose nuts
Powder Coating
Smooth to textured
+60 to +120 µm
Durable, chip-resistant coating across perforated surfaces
Zinc / Nickel Plating
Ra 0.4–1.6 µm
+5 to +15 µm
Galvanic corrosion defense for steel chassis panels
Anodizing (Type II)
Ra 0.8–1.6 µm
+5 to +25 µm
Electrochemical oxide barrier with vibrant dye colors for aluminum

Why Choose Us

Engineers choose Enstark punching for high-speed repeatability and rock-bottom per-part costs on hole-dense components.

/01
High Quality Parts
Hole centerlines hold ±0.1 mm across the sheet. Precision-ground punches ensure sharp edges, low burrs, and tight tolerances verified by pin gauges.
High Quality Parts
/02
Fast Lead Time
Punched parts ship in 3–5 business days. Turret rates exceeding 500 hits per minute drastically outpace laser cutting on perforated panels.
Fast Lead Time
/03
Engineering-Driven Support
We match hole geometries to our extensive standard tool catalog, eliminating unnecessary tooling fees before production begins.
Engineering-Driven Support

What is Sheet Metal Punching?

Sheet metal punching is a high-speed CNC shearing and forming process. A hydraulic or servo-electric ram forces a hardened tool punch through sheet metal into a matching die, creating holes, slots, or raised 3D features such as louvers and knockouts.

✓ISO 9001 certified quality system
✓Multi-station CNC turret punch presses
✓±0.1 mm hole positioning accuracy
✓Extensive library of standard punches & dies
✓Integrated forming of louvers, embosses & knockouts
✓Comprehensive burr and dimension quality inspection

Pros and Cons of Sheet Metal Punching

Pros of CNC Punching

Fastest for Repeated Holes

A single turret hit punches an entire hole or slot instantly. Perforated ventilation screens and arrays run far faster than laser cutting.

Formed Features in One Setup

Louvers, countersinks, bridge lances, knockouts, and stiffening ribs are formed on the press without secondary operations.

No Heat-Affected Zone (HAZ)

Punching is a mechanical shear process producing zero thermal distortion, edge hardening, or discoloration.
CNC Punching Process

Cons of CNC Punching

Sheet Thickness Restrictions

Optimal for light-to-medium gauges up to 3 mm steel/aluminum and 2 mm stainless steel. Heavy plate requires laser or waterjet.

Tooling Geometry Limits

Unusual, highly intricate custom shapes require custom punch tooling, which can introduce upfront tool expense.

Exit-Side Burrs

Mechanical shearing naturally leaves a micro-burr on the die side of holes, which may require secondary deburring.
frequently Asked Questions.
Frequently Asked Questions
What is CNC turret punching?

CNC turret punching uses a revolving turret holding dozens of punch-and-die sets. The machine coordinates sheet movement and tool selection to punch holes, louvers, and embosses at high stroke rates.

How accurate is sheet metal punching?
What is the smallest hole you can punch?
When is punching better than laser cutting?
What formed features can be made on a turret punch?
What is the maximum sheet thickness for punching?
Does punching leave burrs and how are they handled?
How is sheet metal punching priced?

CNC Punching Technical Resources

View All Articles