Enstark Logo
Sheet Metal Welding Services

Sheet Metal Welding Services

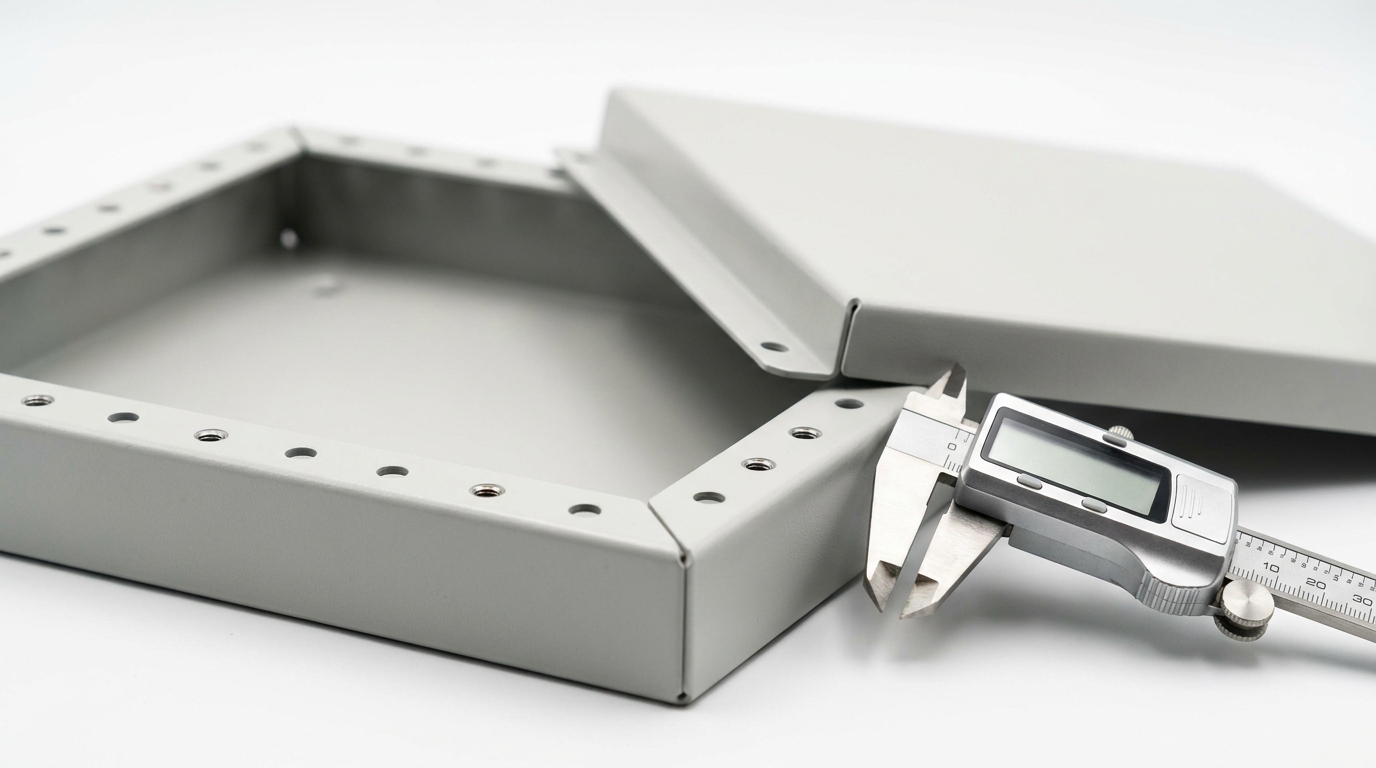
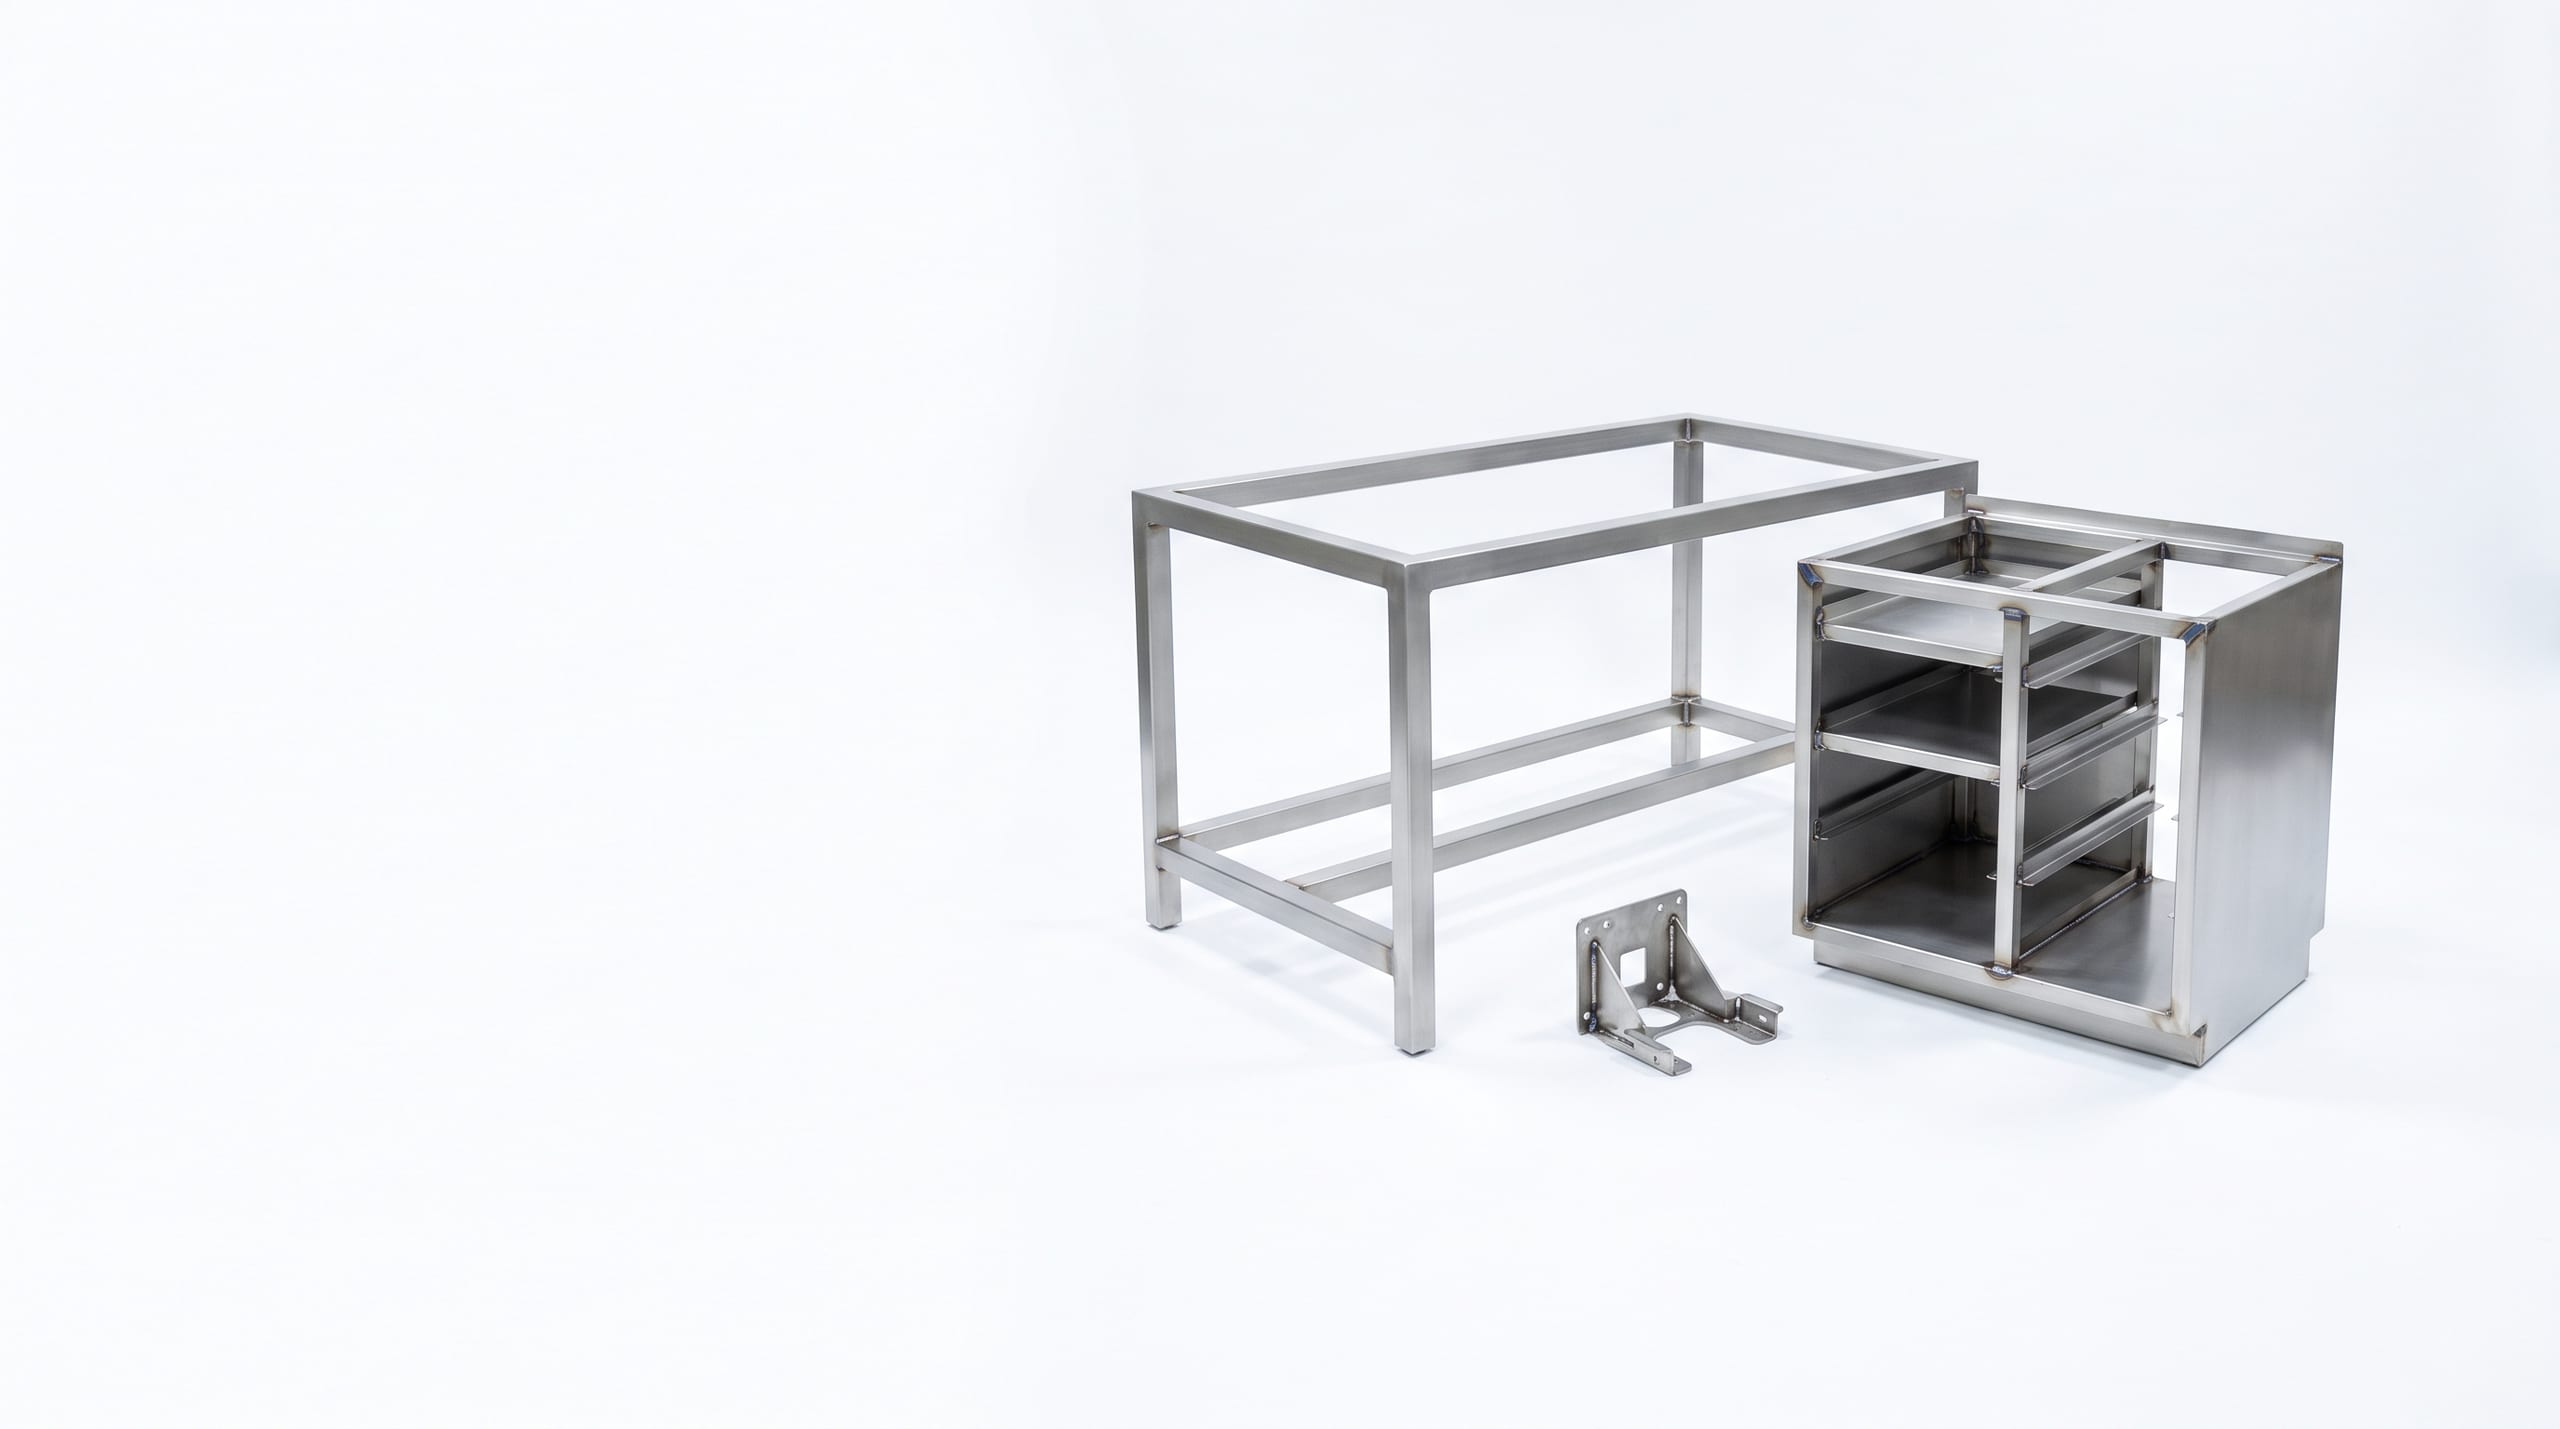
Enstark joins sheet metal assemblies using precision TIG, MIG, spot and handheld fiber laser welding. High structural strength, leak-tight seams and smooth dressed weld surfaces for brackets, frames and enclosures.

✓
100,000+ Parts Made
✓
ISO 9001:2015 Certified
✓
AWS D1.1 & ISO 5817

Get an Instant Sheet Metal Welding Quote

Upload your CAD file for instant pricing and DFM feedback.
Drag & drop CAD files hereSTEP, STP, STL, IGS, IGES, PDF, ZIP — up to 15MB
No commitment required · DFM feedback included
Huawei Technologies
Samsung Electronics
Tata Motors
Delta Electronics
Lens Technology
Eveready Industries
Beijing Institute of Technology
Ansell LTD
NRTC
Chantelle
PT Wings Surya
PT Sun Paper Source
PT Supreme Paper Solution
Huawei Technologies
Samsung Electronics
Tata Motors
Delta Electronics
Lens Technology
Eveready Industries
Beijing Institute of Technology
Ansell LTD
NRTC
Chantelle
PT Wings Surya
PT Sun Paper Source
PT Supreme Paper Solution
Design Guide
Max dimension2000 × 1500 × 1200 mm assembly
Material Thickness0.8–10 mm (laser welding down to 0.5 mm)
Tolerances±0.5 mm overall assembly tolerance
Wall Thickness / Radius
0.8 mm minimum sheet thickness for TIG
Min Feature Size
Weld bead size matching thin component gauge
Surface Finish Options
As-welded, ground flush, brushed, bead blasted, passivated, powder coated
Design advice
1/ Design self-locating tabs and slotsIncorporate laser-cut tab-and-slot features into mating sheets to ensure precise alignment and eliminate expensive welding fixtures.
2/ Use intermittent or staggered weldsOn long joints and thin sheet, stitch or pulse welds prevent heat buildup, minimizing thermal distortion and panel warping.
3/ Specify accessible joint locationsEnsure weld torch nozzles have at least 45° access clearance to joints, avoiding tight internal corners that cause arc wander.

Welding Materials

Our certified welders work across aluminum, stainless steel, carbon steel, and specialty alloys with calibrated filler metals.
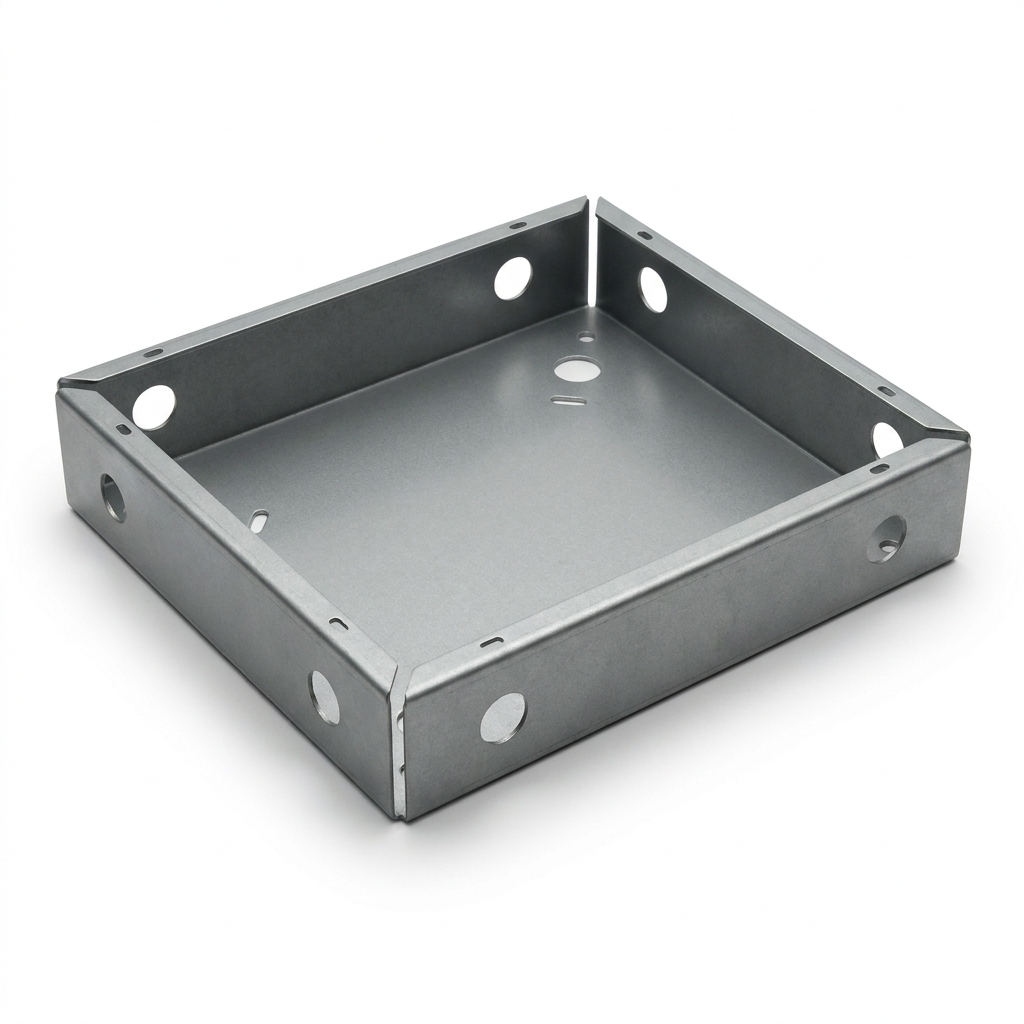
Stainless Steel (304 / 316L)
Welded with 100% argon shielding and matching ER308L/ER316L filler. Outstanding corrosion resistance for chemical, food processing, and marine tanks.
Silver-Gray
Appearance
$$
Price Rating
From 4 business days
Lead Time
Stainless Steel (304 / 316L)
Enstark operates fiber lasers, multi-axis CNC press brakes, turret punches, and robotic welding cells under one unified ISO 9001 quality system.Why Enstark for Sheet Metal WeldingEvery file undergoes upfront DFM review to verify hole-to-edge spacing, bend allowances, and tooling clearances before production starts.
300+Sets of Machine
120+Countries Shipped
20k+Customers Served
Global Shipping World Map
Enstark Online Custom Sheet Metal Service SolutionsGet Quote
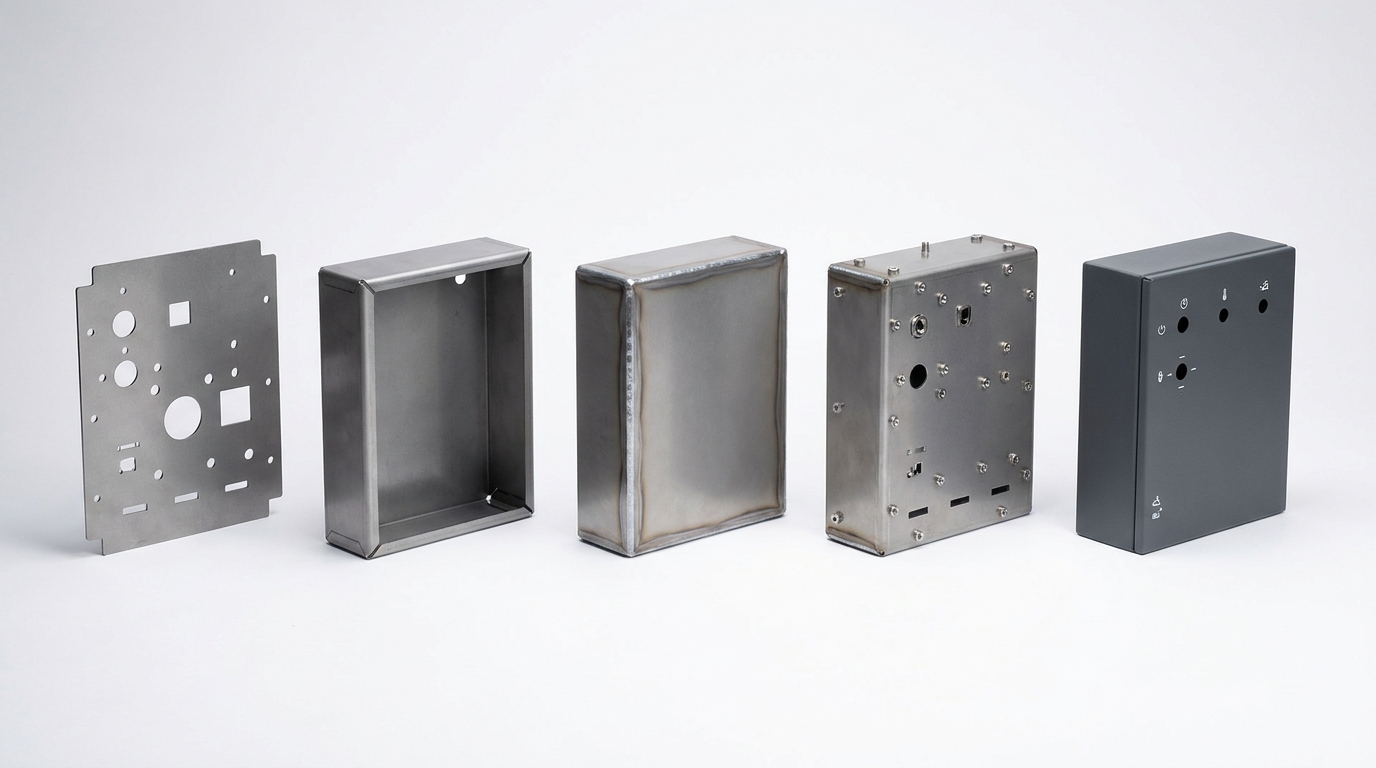
Laser Cutting/01
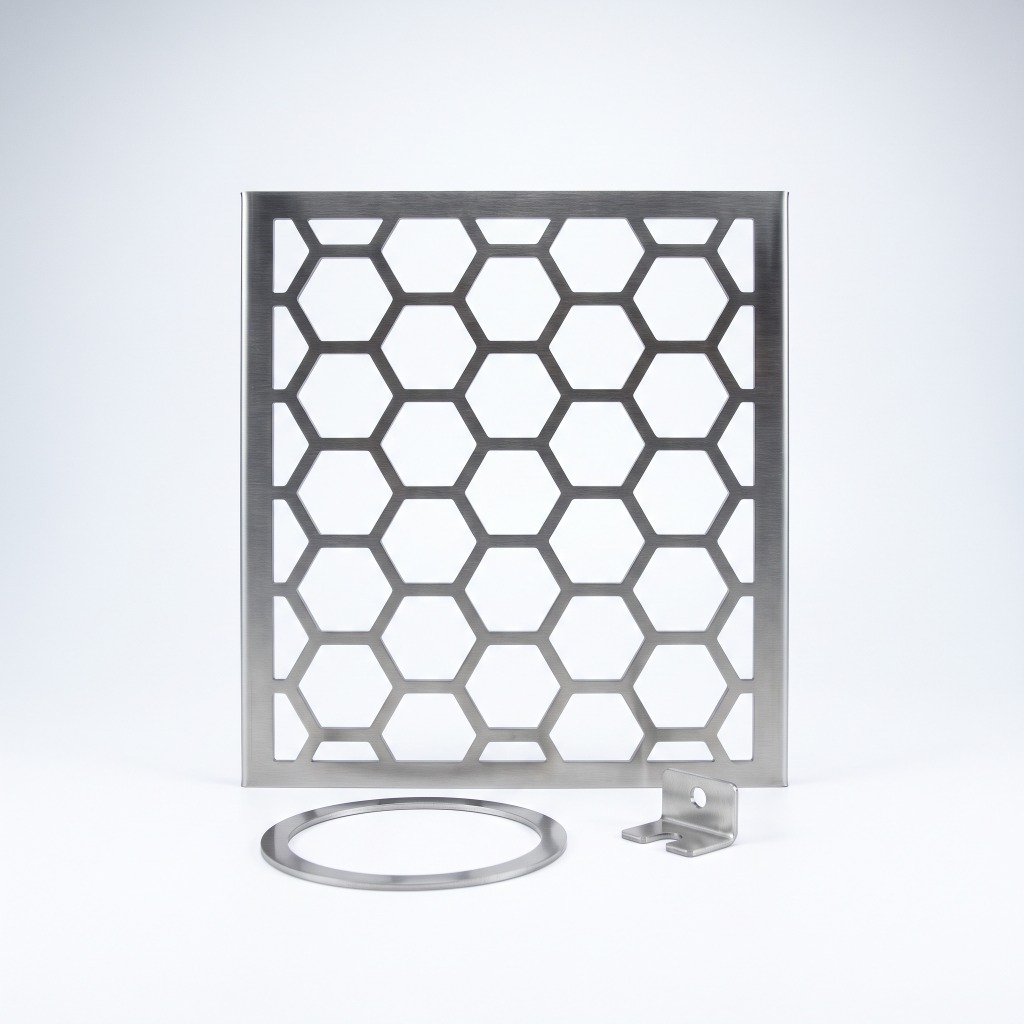
Laser cutting prepares precision edge joints with zero slag and tight ±0.1 mm fit-ups, critical for high-strength welding.
Laser Cutting Solution
CNC Bending/02
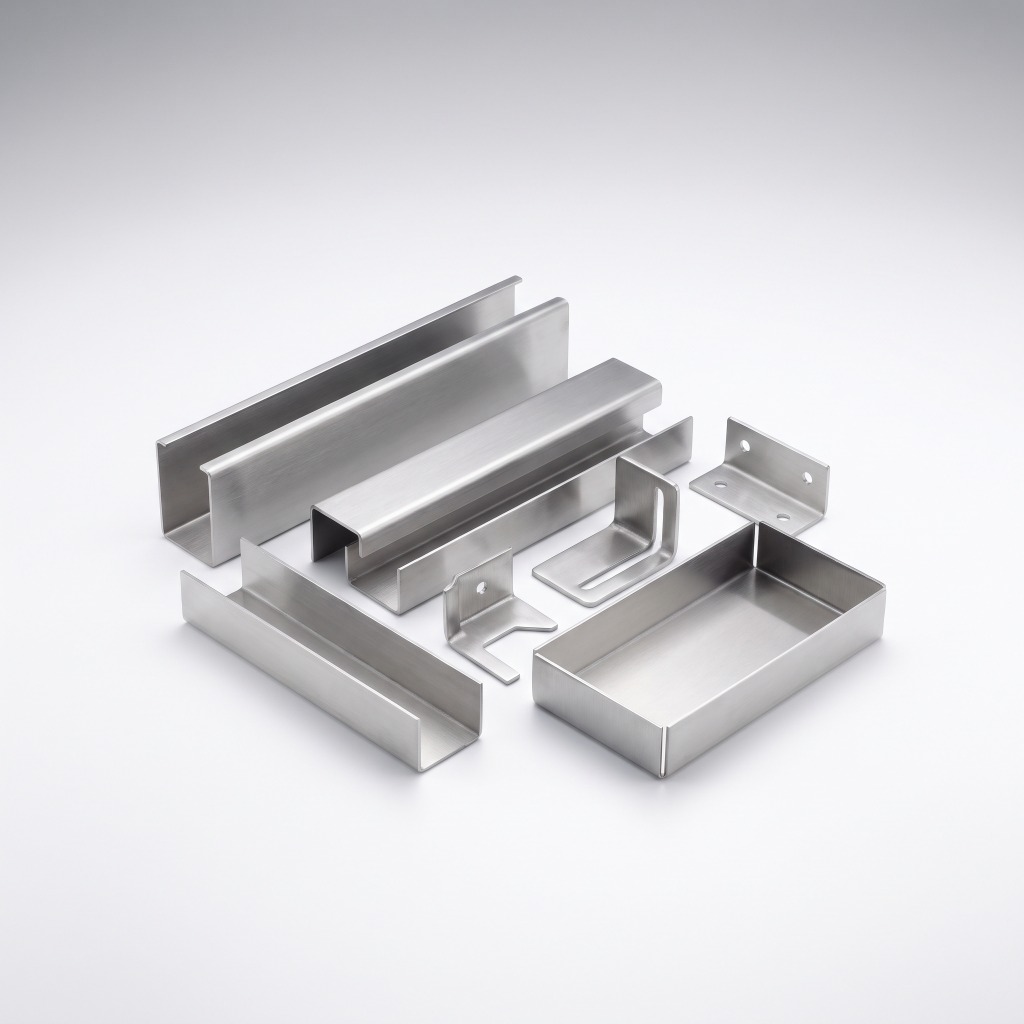
Form panels into structural shapes first to minimize total weld length, reducing assembly labor and heat distortion.
CNC Bending
Sheet Metal Enclosures/03
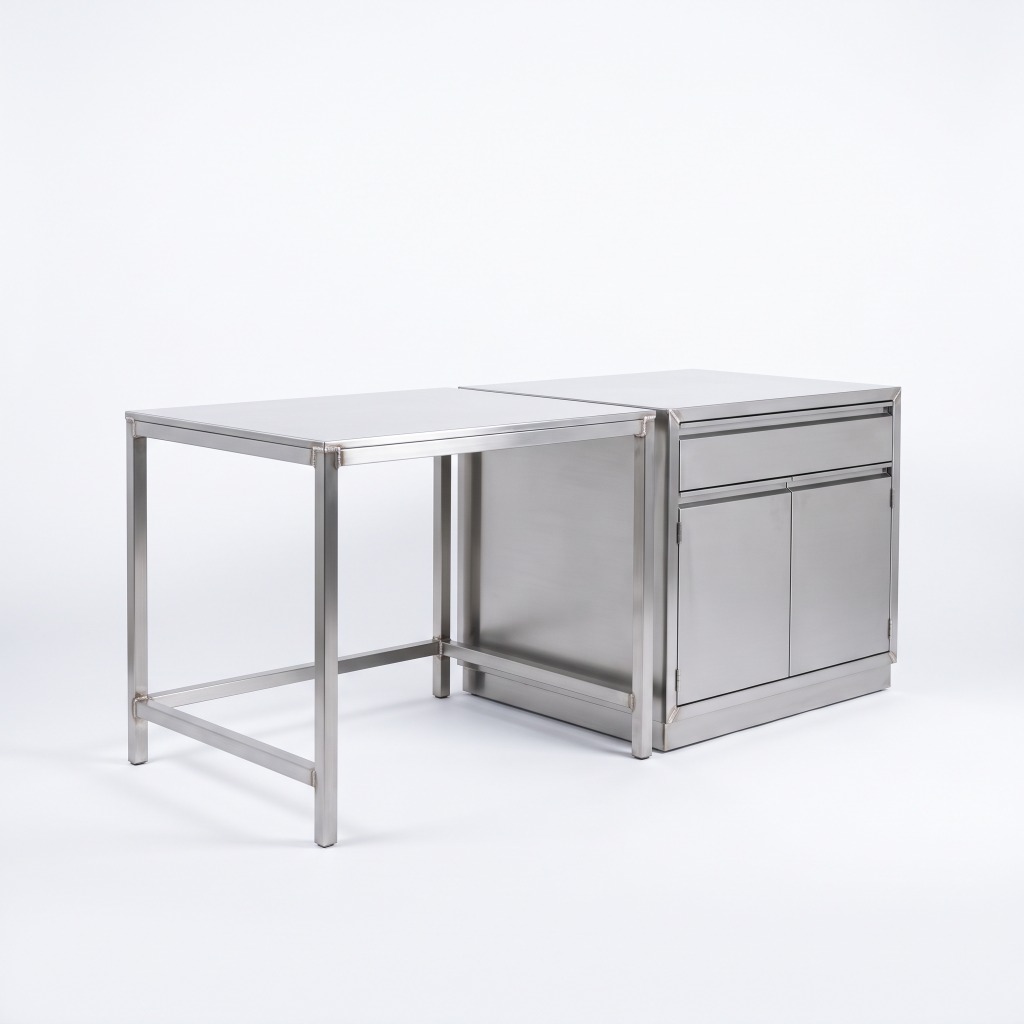
Seamless welded electronic enclosures ground flush, sealed against water ingress, and finished with protective powder coating.
Sheet Metal Enclosures

Welded Part Post-Processing Capabilities

Post-weld treatments to restore corrosion resistance, smooth seams, and prepare surfaces for final coating.

Scroll horizontally to view finishes →
Finishing Process
Surface Roughness
Dimensional Change
Primary Application / Benefit
As-Welded (Cleaned)
Visible uniform weld bead
None
Internal structural weldments where cosmetics are not required
Ground Flush & Blended
Ra 1.6–3.2 µm flush surface
Flushed to parent sheet
Seamless external enclosure corners ready for prime/paint
Pickling & Passivation
Parent sheet texture
Chemical micro-etch
Restores stainless steel chrome oxide layer and eliminates weld discoloration
Bead Blasting
Uniform satin matte
−0.01 mm
Blends heat-affected zones and provides an even mechanical key for coating
Powder Coating
Smooth or textured
+60 to +120 µm
Complete environmental encapsulation and RAL color matching
Zinc Plating
Ra 0.4–1.6 µm
+5 to +15 µm
Economical galvanic rust protection for steel frames and brackets

Why Choose Us

Engineers trust Enstark welding for leak-tight joints, clean seams, and tight dimensional control.

/01
High Quality Parts
Certified welders adhere to ISO 5817 Level B/C quality criteria, ensuring full penetration without undercut, porosity, or burn-through.
High Quality Parts
/02
Fast Lead Time
Welded prototypes ship in 5–7 business days. Modular fixturing tables enable rapid changeover without dedicated tooling delays.
Fast Lead Time
/03
Engineering-Driven Support
Our engineers review weld joint accessibility, fixturing plans, and heat sequencing during DFM review to prevent post-weld distortion.
Engineering-Driven Support

What is Sheet Metal Welding?

Sheet metal welding permanently fuses metal components by melting the base metals together with an electric arc or concentrated laser beam, accompanied by shielding gas. It produces unified, rigid assemblies from formed sheet components.

✓ISO 9001 certified welding fabrication facility
✓AWS D1.1 structural welding code compliance
✓Handheld fiber laser welding for minimal heat input
✓Robotic spot welding for fast, repeatable sheet joining
✓Dye penetrant and pressure leak testing available
✓Precision in-house seam grinding and corner dressing

Pros and Cons of Sheet Metal Welding

Pros of Sheet Metal Welding

High Structural Strength

Produces permanent, high-integrity joints capable of supporting high mechanical loads and pressurized containment.

Leak-Tight & Hermetic Sealing

Continuous welded seams create IP65+ watertight and dustproof enclosures suitable for outdoor and marine enclosures.

Complex Assembly Geometry

Enables joining multiple complex formed panels, heavy structural ribs, and internal bosses into a rigid unibody.
Sheet Metal Welding Process

Cons of Sheet Metal Welding

Thermal Distortion Risk

Localized heat on thin gauges can cause warping or oil-canning, requiring pulse welding and dedicated fixture clamping.

Post-Weld Dressing Required

Cosmetic enclosures require weld grinding, dressing, and blending before powder coating to achieve seamless outer corners.

Permanent Non-Disassembly

Welded joints cannot be taken apart for maintenance, unlike bolted or PEM hardware assemblies.
frequently Asked Questions.
Frequently Asked Questions
What welding processes do you offer for sheet metal?

We offer TIG (GTAW) for precision aesthetic seams, MIG (GMAW) for high-strength steel frames, resistance spot welding for overlapping sheets, and handheld fiber laser welding for ultra-thin low-distortion joining.

What is the minimum sheet thickness you can weld?
How do you prevent heat distortion on thin sheet metal?
Can you grind welds flush for cosmetic parts?
What welding quality standards do you follow?
Can you weld aluminum sheet metal?
Do you offer leak testing for welded tanks and enclosures?
What file information is needed for welded assemblies?

Sheet Metal Welding Technical Resources

View All Articles